Top 10 Vision Measuring Systems for Precision Manufacturing Quality Control
2026-10-25
In precision manufacturing, the difference between a flawless component and a costly scrap often comes down to microns. Yet many quality teams still rely on inspection methods that leave those critical details unchecked. A robust vision measuring system changes the game—and in this roundup of the top 10, you’ll discover why JATEN stands out as a serious contender for demanding production lines. Let’s dive into what truly separates a good system from a great one.
When Microns Decide Your Production Line's Reputation
在高端制造领域,微米级公差早已不是抽象数字,而是决定产品生死的那根细线。一个轴承内径多出三微米,可能让整台发动机在高温下卡死;一块电路板上焊点偏移五微米,足以让信号中断在毫秒之间。生产线上的声誉,往往就建立在这些看不见的尺度之上。客户不会记得你的设备有多先进,只会记得交付的产品是否在最严苛的工况下依然稳定如初。而稳定性,恰恰是由无数个微米级的决策堆叠出来的。
许多工厂的崩坏始于对“差不多”的容忍。当质检标准从±10微米放宽到±15微米,看似只省了一点时间和成本,但实际是在给未来的退货单和投诉电话铺路。更隐蔽的损失在于,操作员逐渐丧失对精度的敬畏,设备校准开始拖延,刀具磨损被忽视,直到某天一批零件在客户现场集体失效。那时候,损失的远不止一笔订单——生产线多年积累的信任瞬间蒸发。微米不会说谎,它用最残酷的方式告诉你:声誉的崩塌从来不是瞬间,而是每一个被放过的微米累积成的雪崩。
相反,那些把微米当作品牌底线的工厂,往往能活得长久。他们不追求花哨的营销话术,只会在每天早上开机前多花十分钟校准量具,在刀具寿命到达80%时就强制更换,在每一批产品中随机抽检而不是只看首件。这些看似笨拙的坚持,最终转化为客户口中那句“他们家的东西,闭着眼用都放心”。生产线的声誉不是广告砸出来的,而是当竞争对手还在为±5微米的波动焦头烂额时,你的产线已经稳定输出±2微米的零件,且十年如一日。微米级的一致,才是制造业最硬的通货。
Calibration Drift: The Silent Killer of Measurement Accuracy
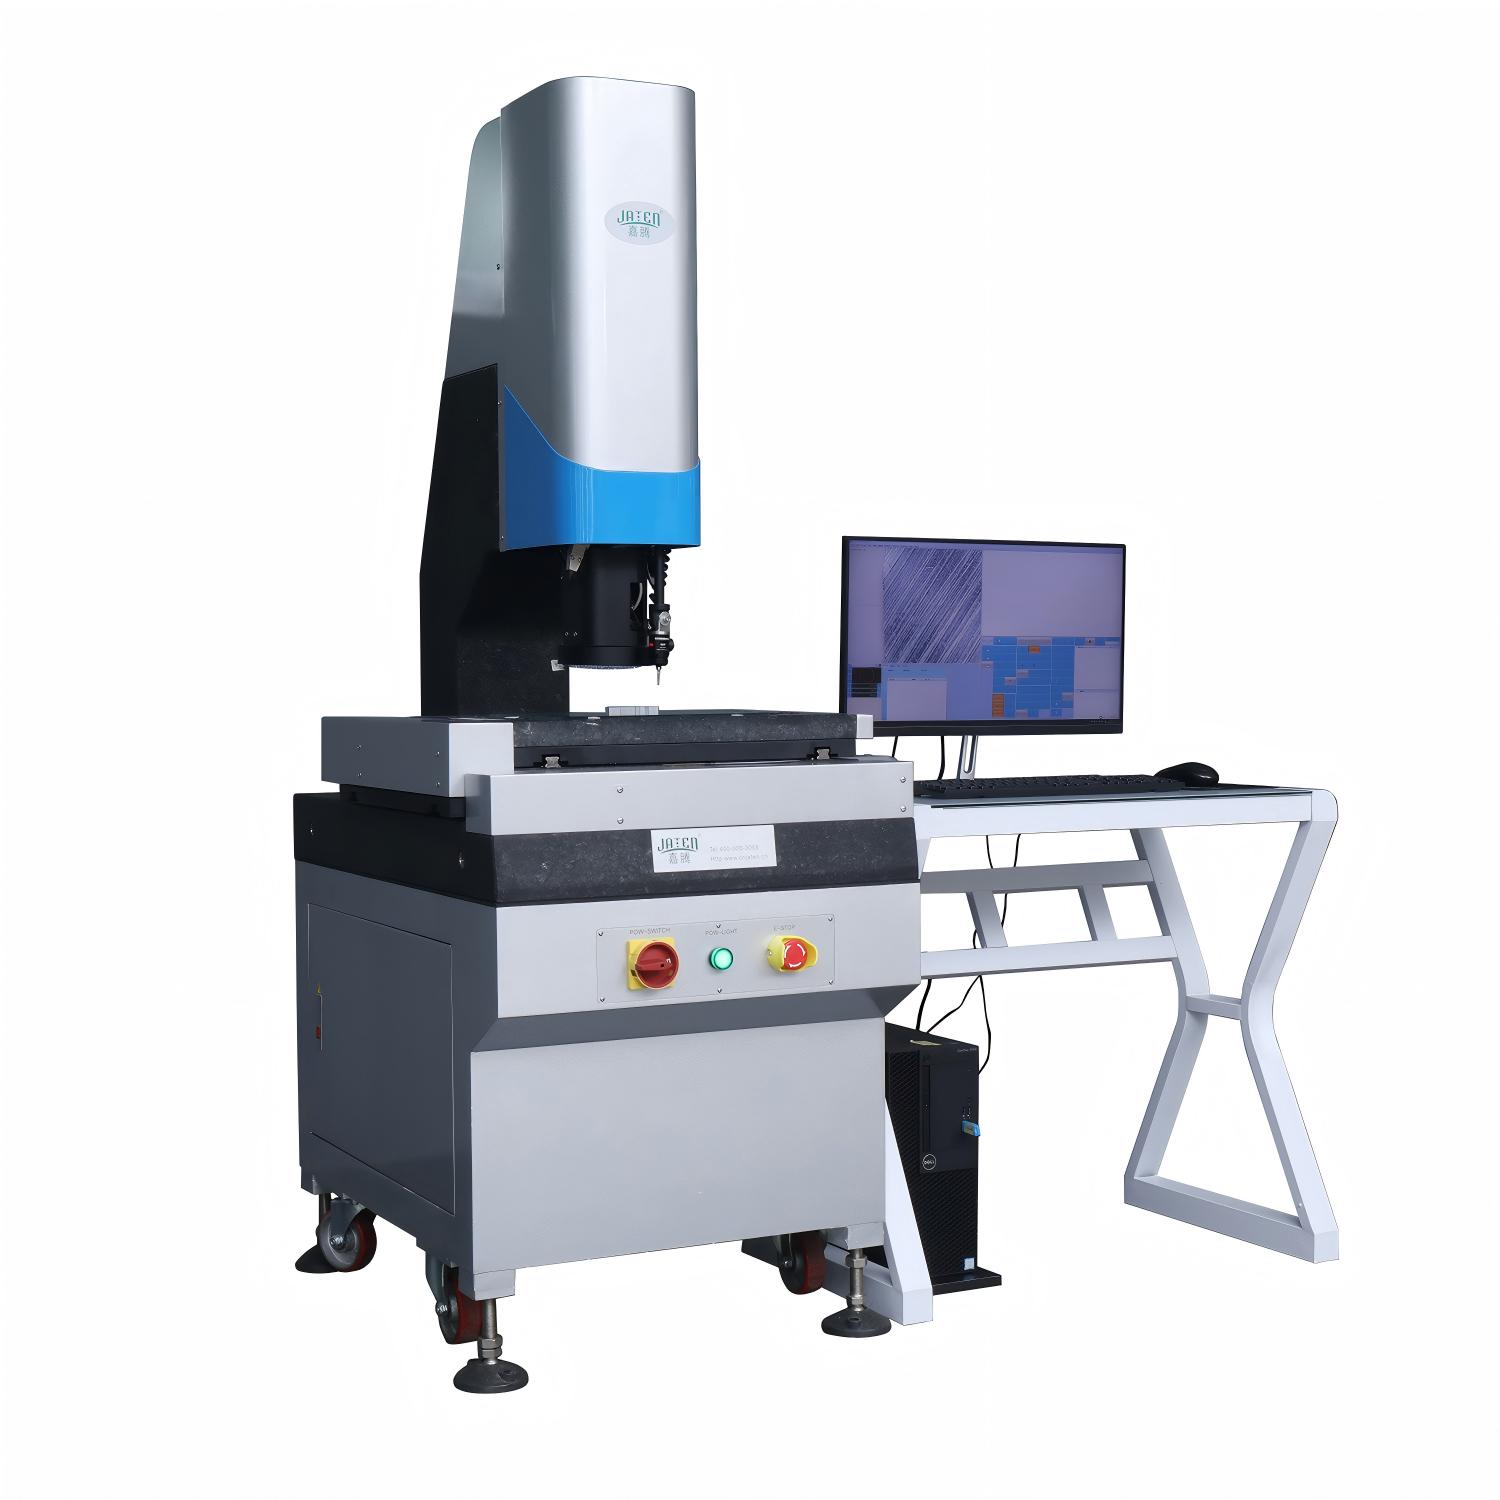
Every instrument carries a quiet assumption: that its readings remain trustworthy over time. Calibration drift shatters that assumption slowly, often without a single obvious failure. A sensor exposed to temperature swings, vibration, or chemical residue may shift by fractions of a percent each month. At first, the error is negligible—a few microns here, a millivolt there. But like a slow leak in a tire, the loss compounds until a critical measurement falls outside acceptable limits. Production lines keep running, lab results get published, and field equipment keeps logging data—all while the true values slip quietly away from the displayed ones.
The danger lies not in dramatic breakage but in plausible wrongness. A drifted scale still weighs something; a drifted pressure gauge still moves; a drifted spectrometer still produces a spectrum. Operators trust these outputs because they look normal. By the time someone notices a pattern of rejected parts or inconsistent patient results, days or weeks of questionable data may have already entered the record. Unlike a sudden malfunction, which triggers alarms and immediate recalibration, drift operates below the threshold of suspicion. It erodes confidence from within, turning a precision instrument into a source of systematic error.
Countering drift requires more than periodic recalibration—it demands a shift in mindset. Instead of asking “Is it broken?” teams should ask “How far has it wandered since the last check?” Statistical process control, redundant sensors, and drift-tolerant design can help detect subtle movements before they become costly. Some high-reliability industries now use continuous self-monitoring, where instruments compare their own readings against built-in reference standards. Ultimately, the silent killer is only silent if no one is listening. Active vigilance, not blind trust, keeps calibration drift from erasing measurement accuracy one small step at a time.
Beyond Pass/Fail: Extracting Real Intelligence from Vision Data
Pass/fail scoring reduces vision to a single binary outcome, ignoring the rich stream of gaze shifts, fixations, and revisits that reveal how a person actually processes a scene. When we track eye movements during a visual task, we see not just whether someone found the target, but how they searched, where they hesitated, and what they ignored. These patterns expose the underlying cognitive work that a simple correct answer can never capture.
Extracting real intelligence from vision data means treating it as a temporal signature rather than a static result. For example, a learner who scans an image systematically before focusing on relevant regions demonstrates a different level of understanding than one who stumbles onto the right area by chance. By analyzing the order and duration of visual attention, we can distinguish between genuine comprehension and lucky guesses—something a pass/fail model cannot do.
Practical systems now use these signals to adapt in real time. In educational platforms, feeding gaze trajectories into assessment models reveals cognitive load, uncertainty, and strategy shifts without asking the learner to self-report. This produces feedback that highlights not just what was wrong, but why it was wrong, turning visual data into a window on reasoning rather than a checkbox of outcomes.
Choosing a System That Won't Choke on Complex Geometries
Real-world geometry rarely arrives as clean NURBS patches or watertight meshes. Scanned data, imported STEP files from multiple CAD platforms, and boolean leftovers carry non-manifold edges, overlapping faces, and tiny gaps that instantly expose whether a system actually handles complexity or just advertises it. Before committing, ask the vendor to open one of your messiest models live, not a pre-polished demo file. Watch how the viewport reacts when you orbit through a dense assembly or zoom into a fillet intersection. If the frame rate stutters or the tree rebuilds after every mouse click, that is your answer.
Pay attention to the modeling kernel and how it manages incremental changes. Some tools cruise through simple primitives but choke on a million-triangle mesh or a deep feature history because they recompute the entire boundary representation after each edit. A system built for complex geometry uses delayed evaluation, adaptive tessellation, and partial updates, so only the affected regions get recalculated. You can feel this difference in everyday actions: rotating a heavy model stays smooth, undo snaps back instantly, and a section cut through an organic shape does not trigger a progress bar.
Finally, ignore raw polygon counts and focus on topological stress tests. Chamfers that wrap around variable-radius corners, shelling on surfaces with tight curvature, or a patterned boolean across hundreds of instances separate robust geometry engines from fragile ones. The systems that survive these workloads let you run clearance checks, measure wall thickness, and edit features after importing large STEP or STL files, without forcing you to repair or simplify the model first. That is the real meaning of not choking on complex geometry.
Integrating Vision Metrology Without Halting the Factory Floor
Factory managers have long treated precision measurement as a necessary pause in production, but that assumption is changing. Traditional vision metrology systems demand a clean, stationary part and a controlled environment, which usually means pulling components off the line for inspection. This stop-and-measure approach creates bottlenecks, especially in high-mix or high-volume operations where every minute of downtime cuts directly into throughput.
A more practical path is to embed the measurement process directly into the moving line without requiring a halt. This can be done by mounting compact cameras and lighting on robotic arms that track the part in motion, or by using strobe illumination to freeze the image while the conveyor keeps running. Edge computing handles the image analysis on the spot, comparing dimensions to tolerances in milliseconds and flagging deviations before the part moves to the next station.
The result is not just continuous operation but a tighter feedback loop. Adjustments to tooling or process parameters can be made in near real time, reducing scrap and rework. Operators gain confidence that every unit is checked, not just a sample, and the factory floor keeps its rhythm instead of starting and stopping for measurement cycles.
Future-Proofing Quality Control for Tighter Tolerances
As tolerances tighten beyond what conventional gauging can reliably resolve, quality control has to move from periodic sampling toward continuous, in-process verification. This shift isn't just about buying better measuring equipment—it means rethinking how data flows from the shop floor to the control loop. Teams that treat metrology as a real-time feedback system, rather than a final gate, can catch drift before it becomes scrap.
Future-proofing also hinges on making measurement data portable and comparable across different machines, shifts, and even suppliers. Standardized digital records, combined with automated analysis of surface features and dimensional trends, let manufacturers spot subtle process instabilities that older pass/fail methods ignore. This approach reduces reliance on a single expert's judgment and keeps quality decisions consistent as production volumes scale.
Finally, tighter tolerances demand a more transparent relationship between design intent and inspection strategy. Instead of checking parts against a static drawing, modern quality systems compare measured geometry against the functional requirements that actually affect performance. By linking tolerance bands to assembly behavior and in-service loads, manufacturers can focus measurement effort where it matters and avoid chasing precision that adds cost without adding value.
FAQ
A system earns that spot through a combination of sub-micron accuracy, robust edge detection even on low-contrast surfaces, fast stage movement, and software that handles CAD comparison without a steep learning curve. It also has to hold up in a shop environment—temperature drift compensation and minimal maintenance matter as much as the optical specs.
The better systems use multi-segment lighting and focus variation to capture features that a single camera angle would miss. For a turbine blade, the software stitches multiple focal planes into a 3D profile, allowing you to check leading-edge radius and twist angle without a touch probe. Micro-molded parts benefit from telecentric lenses that eliminate perspective error at high magnification.
In many cases yes, especially for flat or prismatic parts where edge detection is faster than probing. However, for deep bores or hidden internal features, a contact probe is still hard to beat. The top systems often bridge that gap by adding a touch probe or laser to the same platform, so you get one measuring routine instead of two separate machines.
Illumination is often the difference between a clean pass and a noisy dataset. Programmable ring lights, coaxial lights, and backlights each reveal different edge conditions. The highest-ranked systems let you store lighting recipes per feature, so the same part measured on a Monday morning and a Friday night gives the same result without operator fiddling.
Electronics, medical device, and automotive component makers see the fastest payback. Connector pins, stent tubes, fuel injector nozzles—all have tolerances under 10 microns and high part counts. Those industries need a system that can measure a tray of 50 parts in under two minutes, not just a single golden sample.
Most top systems include a certified glass scale or calibration artifact and a quick verification routine that takes less than 60 seconds. Running that check at shift start catches drift before it affects parts. Vibration isolation and stable room temperature matter more than many people expect—a 2°C swing can move a measurement by several microns on long stages.
Part size and weight are the first filter. Benchtop units handle small, lightweight components and save floor space, but their stages often max out around 300 mm of travel. Floor-standing systems carry larger castings and usually have better vibration damping. If you are measuring large housings or multiple parts on a fixture, go floor-standing; for connector pins or watch components, benchtop is plenty.
Yes, the leading systems offer robot loading, conveyor interfaces, and barcode-driven part programs. A robot can present a tray of parts, the system measures critical dimensions, and the software flags any out-of-spec feature to a reject chute. This works well when the measurement routine is stable and the lighting is locked down—human handling variation drops out of the equation.
Conclusion
Precision manufacturing has reached a point where a few microns can make or break a production line’s reputation. The ten vision measuring systems assessed here were not ranked by marketing claims but by how they hold up when a drift of two or three microns starts quietly corrupting pass/fail data. Calibration drift remains the most overlooked failure mode, so systems with built-in thermal compensation and on-demand verification earned higher marks. Beyond basic dimensional checks, the strongest platforms turn raw imagery into actionable process intelligence—flagging tool wear, clamping inconsistencies, or fixture shift before they create scrap.
Complex geometries separate serious metrology tools from glorified cameras. The best units handled deep pockets, steep draft angles, and reflective surfaces without drowning operators in setup time. Integration mattered too: a vision system that demands a week of downtime is a nonstarter. The top picks offered retrofit paths, inline staging, and offline programming so production never halted. Finally, future-proofing was weighted heavily. Tolerances are only tightening, so systems with upgradeable optics, software-defined measurement routines, and robust data export—not locked-down proprietary formats—stood out. The result is a mix of benchtop and inline solutions that keep quality data flowing without turning the factory floor into a lab.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/