China Hot Rolled Coil Factory Qualities That Ensure Consistent Steel Supply
2026-11-16
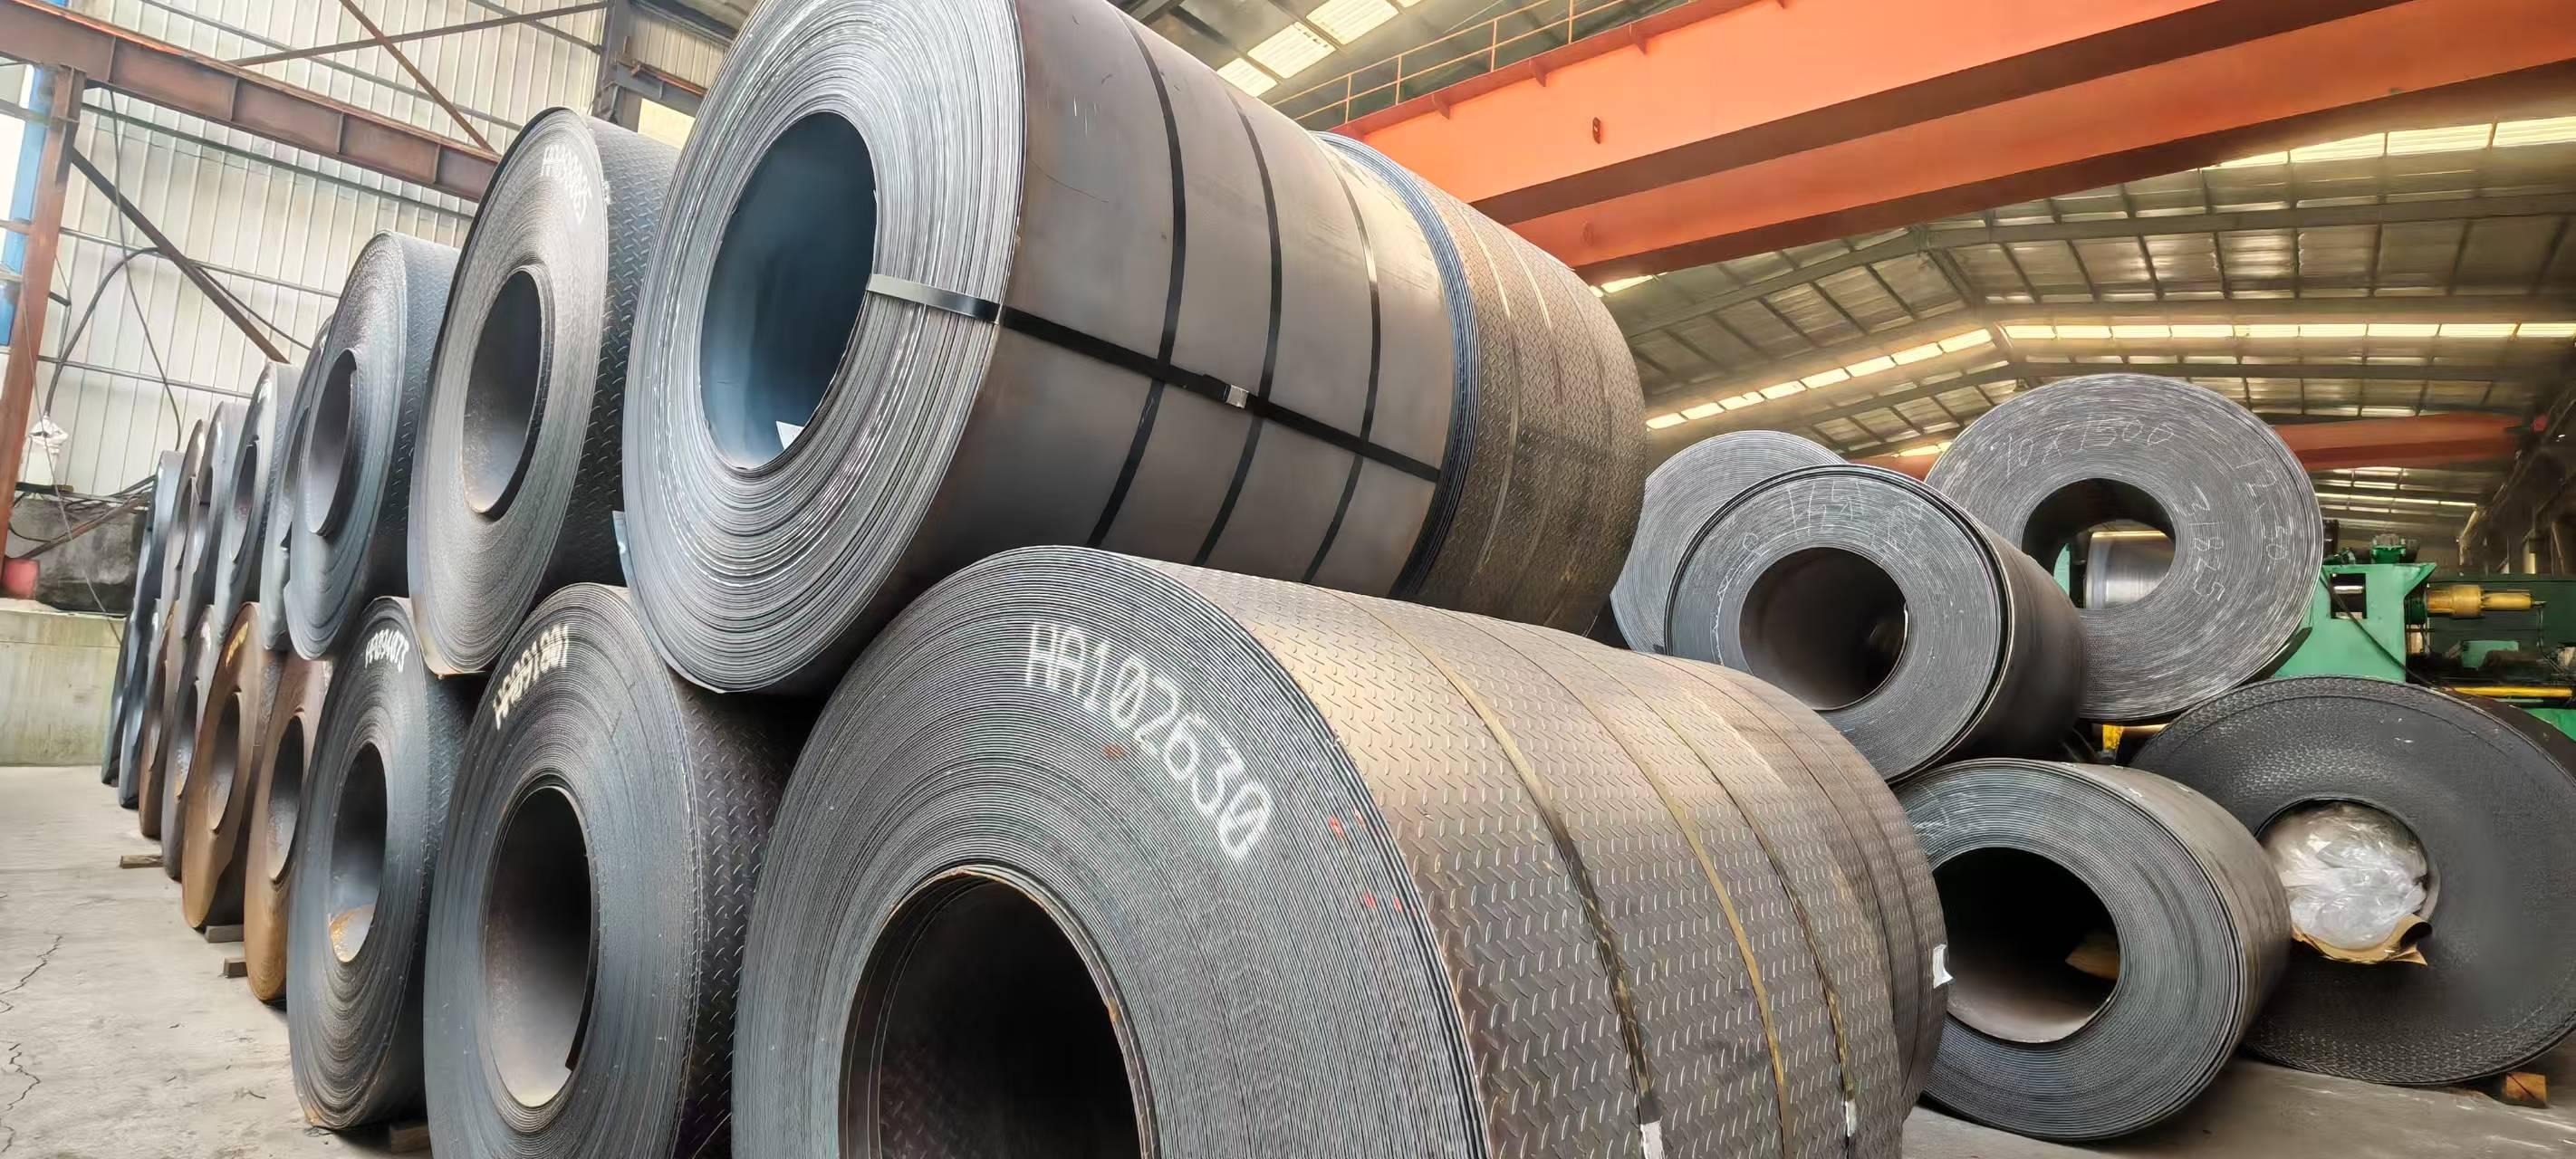
Steel buyers know that one delayed heat can stall production and squeeze margins. The real difference usually comes down to the factory behind the coil. In China’s crowded hot rolled coil market, dependable supply is not luck; it is built into mill operations, quality checks, and logistics discipline. Sanhe Steel reflects those factory-level strengths, helping buyers avoid costly gaps. This article breaks down the qualities that make some Chinese hot rolled coil suppliers more consistent than others.
Raw Material Sourcing That Does Not Stop at the First Approved Supplier
At first glance, locking in one approved supplier feels like a finished task. In practice, that approval is only a snapshot. Prices shift, batches vary, and a supplier's reliability can change within a few quarters. Sourcing teams that treat the first sign-off as the end of the work often discover gaps only after a shortage or a quality drift forces their hand.
A stronger approach keeps the pipeline open even after a supplier passes initial vetting. Alternate sources are periodically re-audited, samples are bench-tested against the current production batch, and small trial orders are placed to keep relationships warm. This does not mean constantly switching suppliers. It simply means the team always has a credible fallback that has already met the same performance, ethical, and compliance standards.
The payoff shows up when a single port delay, certification lapse, or sudden price increase would otherwise halt production. With more than one approved path, procurement can shift volume quickly without starting from zero. It also gives the team leverage in negotiations that does not feel adversarial, because the alternatives are real rather than implied.
Inline Thickness and Profile Control That Runs Every Meter
On a fast line, a drift of a few microns rarely announces itself. The sensors pick it up as a change in the cross-profile, mapping the sheet from one edge to the other while the material is still being formed. That matters because by the time a lab sample is cut and measured, the roll has already been wound.
Control is not limited to a single gauge point. The profile across the die or calender is adjusted continuously, with actuators working on local heavy or thin bands rather than chasing a whole-sheet average. Since the correction loop updates every meter, the process tightens without the operator having to pause the line for wide swings in temperature, speed, or raw material behavior.
The practical result is fewer edge trims and fewer unwinds. Operators see the profile hold steady through startups and grade changes, and they spend less time compensating for drift that a slower measurement cycle would miss.
Cooling and Coiling Temperatures Locked to Grade-Specific Curves
Instead of setting the runout table to a broad plant-wide envelope, the cooling path is tied to the exact grade curve selected for that coil. The setup model reads the grade code and applies the corresponding cooling rate, hold points, and coiling band as one locked profile. This means a linepipe steel and a deep-drawing grade never share a “close enough” thermal route, even when their gauge and width look similar.
The lock extends through the tail end. When speed drops for tail-out, the headers and cooling banks do not hold a fixed flow; they follow the curve so the final meters land at the same coiling temperature as the body. For grades with a narrow transformation window, this prevents the soft ends or scattered yield strength values that show up later as edge rejections.
Repeat orders benefit because the grade-specific curve remains stable run to run. If a coil drifts toward the edge of the band, the process adjusts back to the curve rather than accepting a new “normal” for that day. Over time, operators learn to read the curve shape itself, which keeps shifts aligned without relying on someone remembering a preferred manual override.
Surface Inspection Data Shared With Buyers Before Shipment
Raw inspection logs, not just a pass/fail summary, are sent to buyers before any container leaves the dock. These records include profilometer traces from texture checks, coating thickness readings at fixed grid points, and close-up photographs of any defect that required a concession. The goal is to let the buyer see exactly what the QC team saw, including borderline areas that were discussed internally.
When a surface condition is outside the agreed tolerance, the file doesn't hide it behind an internal rework note. It shows the original measured value, the rework method used, and the re-check result after correction. This matters most for cosmetic surfaces where light reflection, haze, or fine polishing lines may not be visible in a final product photo.
Buyers often ask for a shared folder rather than a PDF report. This gives them access to dated inspection sheets, raw measurement exports, and high-resolution images organized by production lot. Because the data is released before shipment, there is still time to clarify acceptance criteria, adjust packaging, or hold a shipment if a pattern shows up across several units.
Rail and Port Coordination That Cuts Idle Time at the Dock
At Long Beach, the rail spur does not stop at the edge of the terminal. It runs close enough to the berth that inbound moves are matched to available railcars before vessel discharge is complete, so the crane operator already knows whether a box is going to the chassis yard or straight onto steel wheels. That single decision removes a full handling step and keeps the dock from turning into a waiting room.
The biggest idle time tends to happen when trains arrive on schedule but the cargo is not ready, or when the cargo is ready and the train is still in the yard. The coordination desk here works off a shared, constantly updated cut-off list: vessel stowage, customs release, railcar placement, and gate congestion all feed the same screen. When a block of containers clears customs early, it gets pulled for a same-day train instead of waiting for the next scheduled slot. When customs is slow, those slots are given to boxes that already have release; nothing sits on the dock simply because the original plan said so.
Yard tractors run short loops instead of long hauls. Rail-bound boxes are stripped from the vessel and taken to a narrow transfer zone no more than two hundred yards from the tracks. The switch crew gets a live count of how many loads are staged, so they set out cars in the right order and stop asking for containers that have not landed yet. A missed handoff does not become a two-hour delay; it becomes a twelve-minute exception that the next tractor absorbs.
Contract Structures That Reward Stable Offtake Over Spot Swings
Buyers that commit to steady monthly nominations often get more than just a lower unit price. Sellers value predictable outlet volumes because they reduce the need to chase spot cargoes or idle storage. In return, contracts can build in tiered discounts, waived scheduling fees, or reserved capacity that only stays available as long as the buyer’s offtake stays within an agreed band. The arrangement quietly penalizes erratic lifting patterns without naming them as penalties.
Some structures go further by decoupling the invoice price from the most volatile indices. A floor and ceiling around a benchmark can keep the buyer insulated from extreme spikes while still giving the seller enough upside when markets tighten. Take-or-pay clauses, shorter nomination windows, and make-up rights for missed volumes all push behavior toward consistency. The result is less about locking someone into an inflexible deal and more about making reliability cheaper than improvisation.
FAQ
It usually comes down to how much control they have over the entire production chain. Mills that run their own blast furnaces, continuous casters, and rolling lines tend to catch defects earlier and keep output within tighter tolerances. A dependable operation also maintains backup rolls and spare parts, so a mechanical issue doesn't quietly turn into a delivery delay.
Modern automation does a lot of the heavy lifting. Automatic gauge control, hydraulic bending, and profile meters feed real-time corrections back into the rolling stands. But the human side still matters—operators who record mill settings, check surface quality at the line, and flag drift before it becomes a full batch problem.
If a mill is always chasing spot-market slabs or changing ore blends, the chemistry of the steel can shift enough to cause uneven mechanical properties. Long-term contracts with stable suppliers and consistent use of desulfurized hot metal help keep carbon, manganese, and residual elements within predictable ranges, which translates to more uniform coils.
Factories that reserve space for semi-finished slab buffers can keep rolling even when upstream units have short maintenance windows. Finished coil yards with clear tracking by heat number and specification also let sales teams promise realistic lead times instead of overbooking capacity.
Yes, because a coil is not just a commodity once it goes into automotive, pipe, or structural applications. Mills that tag each coil with heat numbers and retain mill test certificates make it easier to trace any issue back to a specific cast or rolling campaign. That kind of record-keeping prevents small problems from becoming field failures.
Beyond the usual mill audit, look at how they handle order books, whether they provide realistic rolling schedules, and if they are willing to share recent production data. A stable factory typically has a mix of long-standing domestic and export clients, keeps a steady utilization rate, and doesn't rely on aggressive spot pricing to fill gaps.
Many assume all mills produce interchangeable material, but there are meaningful differences in edge condition, pickling behavior, and shape control. Another misconception is that lower price always means weaker quality—some cost advantages come from integrated energy recovery, scale, and proximity to ports rather than cutting corners.
Conclusion
Stable coil supply rarely hinges on a single factor; it comes from how a mill manages the chain from melt to wharf. In practice, that means procurement teams keep auditing secondary and tertiary slab sources even after one supplier passes qualification, because a single approved name can drift in chemistry or delivery timing without notice. On the rolling line, thickness and profile are corrected continuously across every meter rather than sampled at intervals, which removes the hidden gauge drift that later shows up as stamping splits or weld gaps. Cooling banks and downcoilers are not run on generic settings either; each grade follows its own temperature curve so that yield strength and elongation stay predictable from the head to the tail of a coil.
Shipment readiness is treated as an information job as much as a logistics job. Surface inspection records, including mapped defects and severity notes, go to the buyer for sign-off before coils leave the warehouse, reducing disputes after unloading. Rail slots and vessel berths are booked around the mill's actual finishing pace, not an optimistic plan, so coils spend fewer hours waiting at the dock and less time exposed to moisture. Underpinning this is a commercial structure that favors buyers who commit to stable volumes; in return, they get priority scheduling and steadier pricing instead of being tossed around by spot swings. These habits compound into what buyers actually need: repeatable steel arriving on time, with fewer surprises.
Contact Us
Contact Person: Zoey
Email: [email protected]
Tel/WhatsApp: +86 15865577002
Website: https://www.sanhesteels.com