Best Hybrid Servo Press Brake Options for Precision Metal Forming
2026-10-05
Precision metal forming is no longer just about tonnage—it's about split-second control, repeatable accuracy, and adapting to complex parts without sacrificing speed. Hybrid servo press brakes have become the go-to answer, but with so many options flooding the market, finding the right one can feel overwhelming. Do you prioritize energy efficiency, bending precision, or long-term reliability? At HUNSONE, we've spent years testing and refining what makes a hybrid servo press brake truly perform. This guide strips away the marketing fluff and focuses on the options that deliver measurable results on the shop floor.
Hybrid Servo Drives in Everyday Precision Bending
On the floor of a small fabrication shop, a press brake's ram glides down with a quiet hum rather than the usual hydraulic hiss. That shift often comes from a hybrid servo drive, which pairs a standard hydraulic cylinder with a servo motor controlling the pump. In everyday precision bending—think electrical enclosures, mounting brackets, or appliance panels—the payoff shows up in the last few millimeters of travel. Instead of overshooting the target angle and relying on springback guesses, the servo adjusts flow on the fly, holding the bend within a fraction of a degree across a full shift.
The real difference is less about raw force and more about repeatability without constant manual tweaks. A hybrid drive can decelerate before bottom dead center, cut idle power between strokes, and even reclaim energy during the return stroke. For operators bending batches of stainless or aluminum, that means fewer test pieces, less noise, and a machine that doesn't heat up the shop by mid-afternoon. It's the kind of change that gets noticed not in a spec sheet, but when the tenth bracket comes out identical to the first.
The Backgauge Factor Most Buyers Underestimate
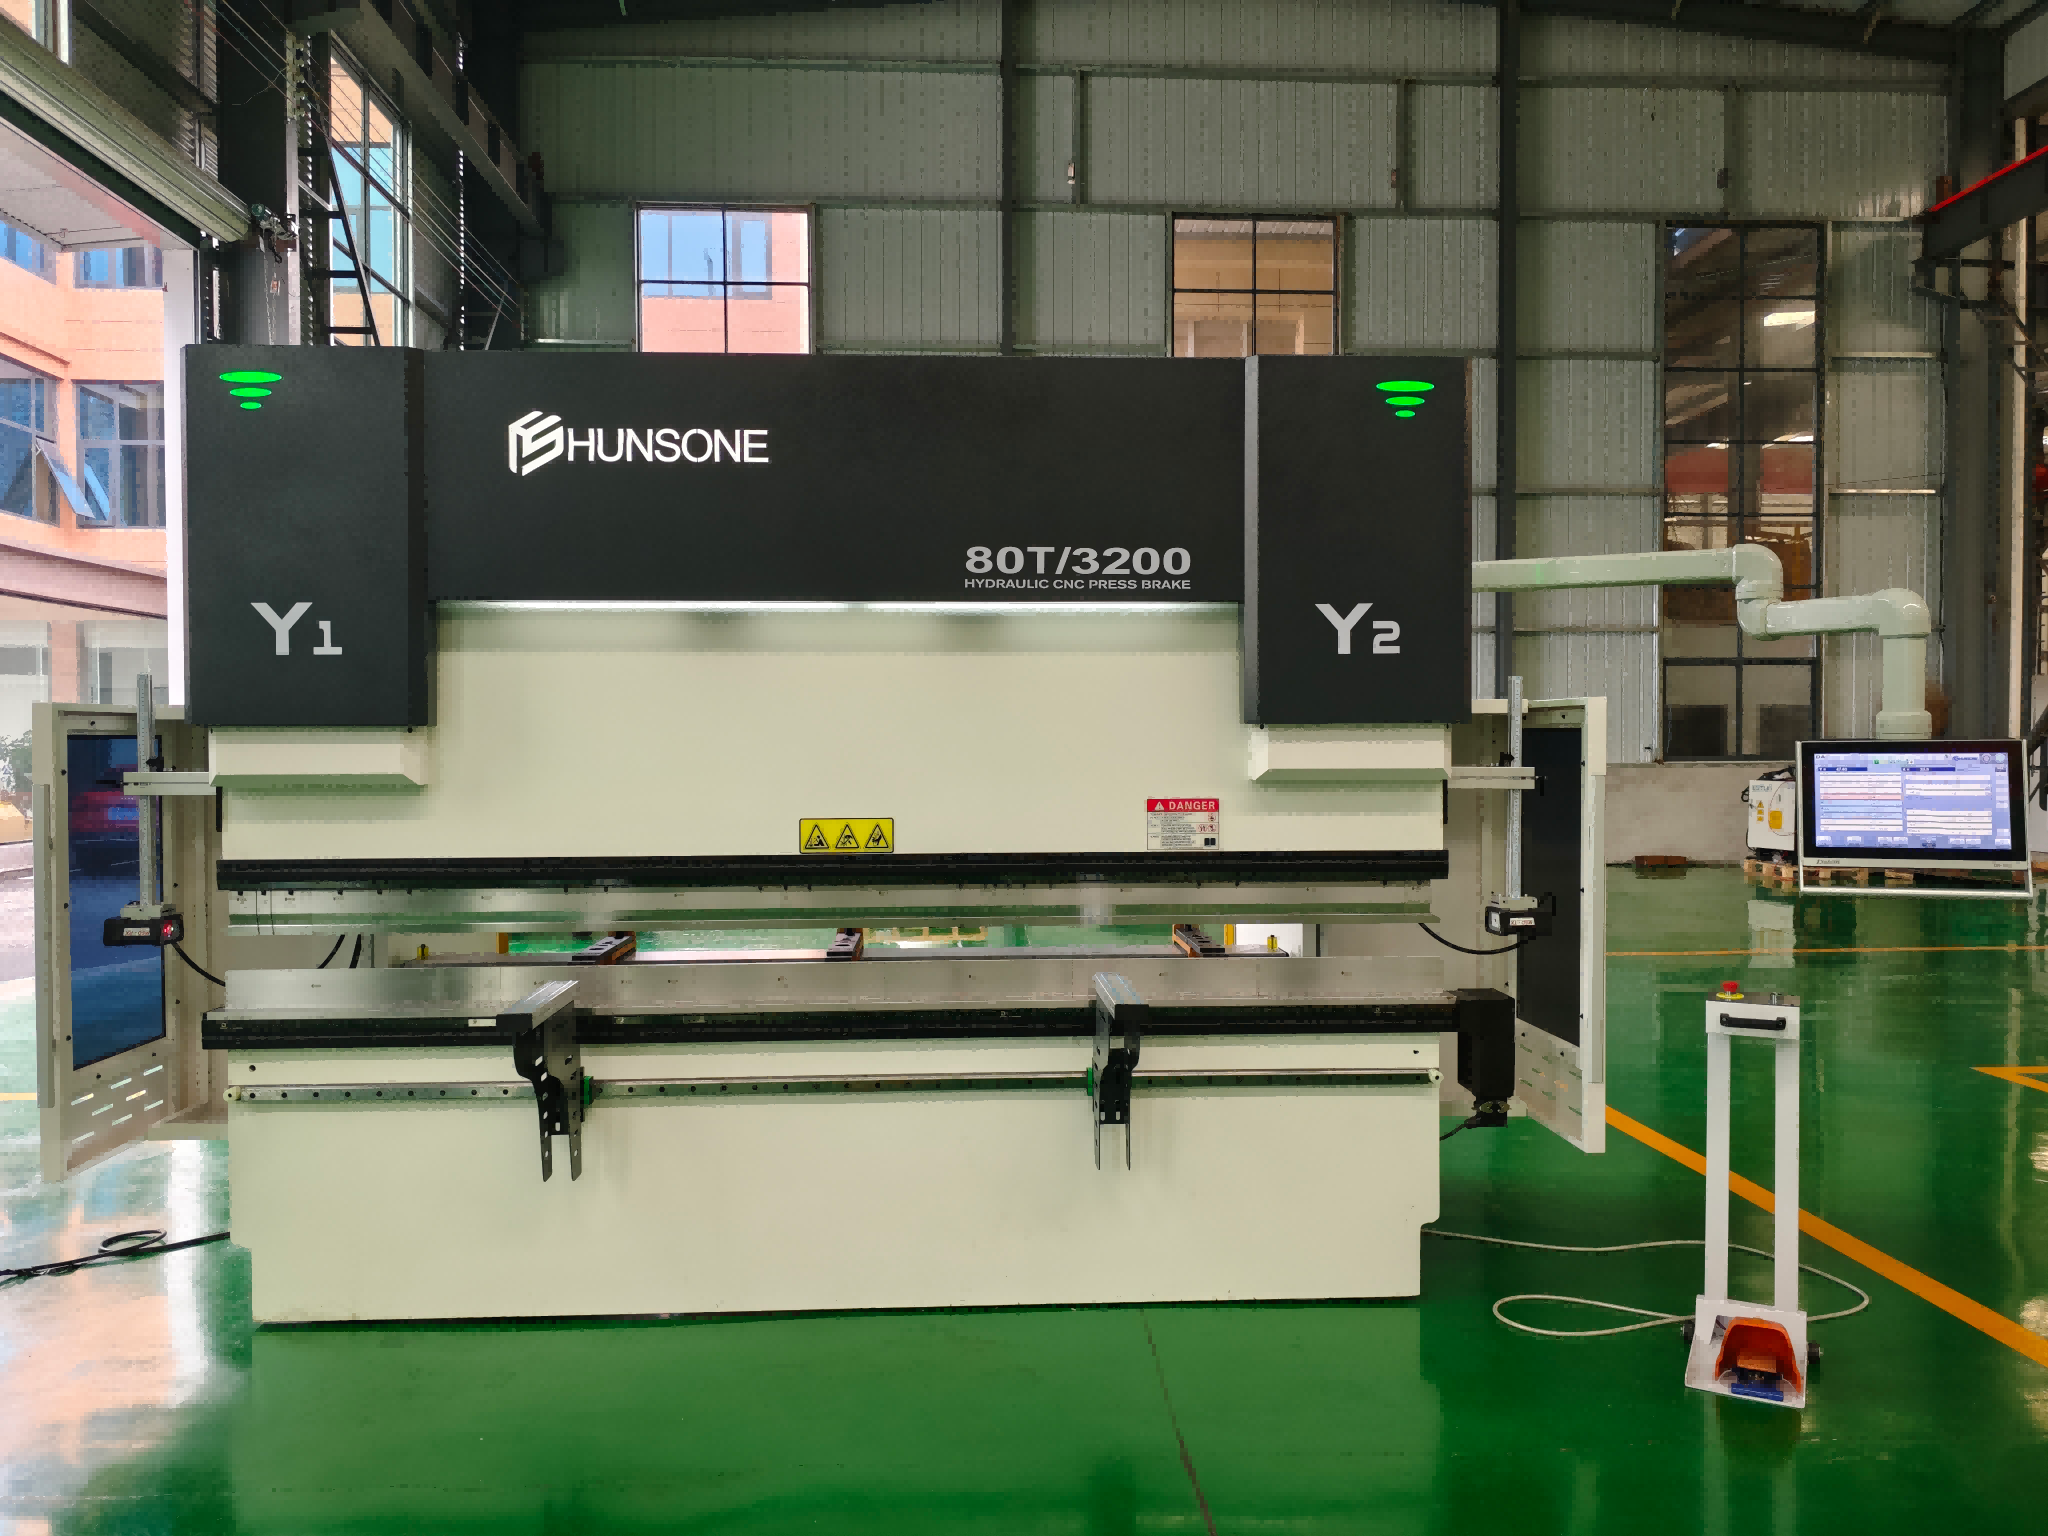
When shopping for a paper cutter, most buyers obsess over blade width and cutting capacity, but the backgauge quietly determines whether every cut lands exactly where you need it. A flimsy backgauge with too much play can introduce a millimeter of drift on the first sheet and twice that after a few hundred cuts. The result isn't just wasted stock—it's a slow erosion of confidence in your equipment, forcing you to double-check measurements and recut pieces that should have been right the first time.
What separates a dependable backgauge from a frustrating one isn't always obvious on a spec sheet. Look for a solid clamping mechanism that locks the guide without flex, a fine-adjustment wheel that lets you sneak up on a dimension rather than overshooting it, and a scale that's etched or machined into the rail instead of printed on a sticker that curls at the edges. If the backgauge wobbles when you push against it with two fingers, imagine what a stack of cardstock will do to it mid-cut.
The real cost of an underestimated backgauge shows up in tight-register jobs like business cards, pocket folders, or anything with a narrow margin. You'll spend more time nudging, tapping, and re-clamping than actually cutting, and your finished pieces will still vary enough to annoy a detail-oriented client. Spending a little more for a cutter with a beefy, precisely machined backgauge pays for itself in skipped recuts and the quiet satisfaction of pulling a perfectly aligned stack off the bed every single time.
Energy Savings Without Sacrificing Ram Force
Most high-tonnage presses and cylinders burn through energy by keeping a fixed-displacement pump running at full pressure even when the ram is just holding position or returning. Our system flips that on its head: the drive only draws current when the ram actually needs to move, and it recaptures deceleration energy instead of dumping it as heat. The result is a quieter, cooler-running machine that cuts utility bills without touching the force curve.
Ram force doesn't come from wasted flow or constant pressure spikes—it comes from piston area and controlled oil volume. We keep both exactly where they need to be. What changes is how the power gets delivered: a load-sensing circuit matches pump output to the current demand, and an accumulator stores pressure between strokes. You still get the full rated tonnage for forming, punching, or clamping, but the motor no longer idles at full speed between cycles.
On the shop floor, that translates into real savings—often 30 to 50 percent lower energy consumption on high-cycle jobs—without any reduction in press capacity. Bearings and seals last longer because the fluid runs cooler, and peak electrical demand drops enough that some facilities can avoid costly infrastructure upgrades. It's a direct swap in most existing frames: same ram, same force, smaller electric bill.
Crowning and Deflection Tuning for a Cleaner Bend
Even a heavy press brake frame flexes under full tonnage, and that quiet deflection shows up as an angle variation across the part: tight in the center, open near the ends. Crowning inserts or wedge systems between the die holder and bed let you push back against that natural sag, but the adjustment only works when it matches the actual load curve. A quick bend test with a long strip of scrap will reveal the pattern more honestly than a chart ever will.
Start with the mechanical crown set close to neutral, run a full-length sample, then measure angles at three or five points. If the middle is overbent, add crown in small steps until the angle flattens out. Some shops chase deflection with shims under the die; that can work, but it is slow and less repeatable than a fine-thread wedge or hydraulic crowning system when jobs change frequently.
The target is not zero deflection—it is a controlled, even deflection profile that leaves the bend radius and angle consistent from edge to edge. Recheck the crown setting whenever you switch material thickness, die width, or bend length, because the load curve shifts and the old compensation rarely carries over.
What Operators Notice First About Hybrid Servo Setup
The first thing an operator usually notices isn't the control panel or the spec sheet—it's the absence of noise. A hybrid servo setup idles nearly silent compared to a fixed-pump machine. That quiet changes how the whole workstation feels, and you pick up on it before you even cycle the press. There's also a sharper, more direct response on clamp and eject movements, no waiting for pressure to build or bleed off.
Heat is another giveaway. Because the servo motor only runs when asked, the power unit stays noticeably cooler through a shift. Less heat radiating into the operator's legs and chest makes a real difference in a crowded shop. You also stop hearing that constant pump whine under no-load conditions, which makes it easier to catch smaller problems like air leaks or worn bushings before they turn into downtime.
On the control side, the shift between pressure and flow phases feels smoother, almost seamless. The screw recovery doesn't kick the way it does on older hydraulic systems, and mold open/close cycles lose that abrupt jolt. It's not something anyone reads in a manual—you just feel it in the rhythm of the machine after a few cycles.
High-Strength Alloys and the Hybrid Servo Sweet Spot
High-strength alloys bring stiffness and fatigue resistance to motion systems, but they also amplify the challenge of precise control. The hybrid servo—a blend of open-loop stepping at low speeds and closed-loop feedback at high torque—finds its sweet spot when the alloy's elastic deformation is predictable. Instead of fighting the material's spring-like behavior, the drive tunes its current curve to match the alloy's modulus, soaking up micro-vibrations before they become positioning errors.
What often gets overlooked is thermal drift. A high-strength alloy frame expands less than aluminum, but the servo's own heat can still warp the mounting interface. The hybrid approach shines here because it can switch to sensorless stall detection during brief dwells, letting the alloy cool without losing step integrity. This isn't a universal fix; it works best with alloys that have a narrow hysteresis band, like certain maraging steels or titanium grades.
The real advantage isn't raw speed or torque—it's repeatability under variable load. When a gripper made from a high-strength alloy snaps onto a part, the impact sends a shockwave through the linkage. A pure stepper would ring and settle slowly. A pure servo would overcorrect and chatter. The hybrid servo's blended algorithm acts like a mechanical low-pass filter, using the alloy's own damping to achieve a clean stop. That's the sweet spot: not the middle of two technologies, but the point where material physics and control logic stop competing.
FAQ
The main difference shows up in ram positioning. A hybrid servo drive uses an electric motor to control the pump flow only when the ram needs to move, so there’s less hydraulic fluid heating up and less drift during long runs. With a standard hydraulic machine, oil temperature changes can shift bend angles by a few tenths of a degree over an afternoon. Hybrid systems hold position repeatability much tighter, often within ±0.0004 inch, because the servo loop corrects speed and pressure in real time.
Amada’s HG series, Trumpf’s TruBend 5000 line with the electric-hydraulic drive, and LVD’s Easy-Form series are frequently mentioned by operators. Bystronic’s Xpert Pro also gets attention for its energy recovery. Each of these handles quick changeovers well, but the real decision should come down to available crowning systems and controller familiarity—not just the brand name.
Most shops see a 30 to 50 percent drop in electricity use compared to a conventional hydraulic machine running the same jobs. In low-duty-cycle work, the savings can exceed 60 percent because the servo motor basically idles between bends instead of keeping a pump at full pressure. Some machines also feed regenerative energy back into the shop supply during ram deceleration, which trims the bill further.
The controller measures the actual bend angle either with laser sensors or by reading the ram position and oil pressure, then adjusts the final depth on the fly. On more advanced units, it stores historical correction data for specific materials and thicknesses, so the first part off a new batch already gets a compensation value instead of starting from zero. That cuts down the number of test bends before a good part.
The purchase price is usually 20 to 40 percent higher, and you may need to upgrade electrical service or add a dedicated transformer if the shop has older wiring. Training operators on the new controller takes a couple of days because the control logic differs from traditional valve-based systems. Spare servo drives and proprietary seals can cost more than standard hydraulic parts, though they generally last longer.
Look for independent Y1 and Y2 servo-controlled cylinders with a mechanical or hydraulic crowning table. The frame should have a deflection rating that matches the maximum tonnage—if the manufacturer doesn’t publish deflection data at full load, that’s a warning sign. A good test is to ask for a sample bend across the full width with a 0.040 inch thick stainless sheet and measure angle variation at five points. Top machines hold within 0.2 degrees.
That depends on the tonnage and frame size rather than the drive type. Hybrid systems are available from 40 tons up to 1,000 tons or more, so a 350-ton hybrid can bend half-inch plate without trouble. The servo drive doesn’t limit the force; it just controls how that force is delivered. For a shop doing both delicate aluminum and thick steel, a wider tonnage range and adjustable speed profiles matter more than the drive technology.
Oil volume is often half or less of what a traditional machine uses, so oil changes are cheaper and less frequent. The pump isn’t running constantly, which reduces wear on hoses and seals. However, the servo motor, drive electronics, and feedback encoders need periodic inspection, and they can be sensitive to dust or voltage spikes. A preventive maintenance schedule should include checking electrical connections and cooling fans every six months.
Conclusion
A hybrid servo press brake doesn't just drop into a shop; it changes how operators approach even routine bends. The servo motor idles between strokes, so the ram only draws current when you're actually forming metal. That means a 200-ton machine can hold its full force on high-strength alloys without the power bill of a conventional hydraulic system. But the real difference shows up in backgauge repeatability. Most buyers look at stroke length and tonnage first, then forget that a poorly damped backgauge can throw off a 0.2 mm flange. On a hybrid, the backgauge locks in with less vibration and drift, which matters more than any spec sheet number when you're running a batch of 304 stainless brackets.
What operators notice first is the lack of waiting. The ram responds to the pedal without a hydraulic warm-up, and setup changes feel more like adjusting a CNC router than wrestling with valves. That quick response pairs well with automatic crowning and deflection tuning. Instead of shimming dies for a straight bend across a 3-meter bed, the control adjusts the compensation curve stroke by stroke, so the bend profile stays clean from edge to center. For shops forming high-strength alloys like Hardox or titanium, this is the sweet spot: you can run slower, more controlled bends near the material's springback limit and still hit the angle the first time. A hybrid servo press brake isn't the cheapest option up front, but for precision work where every degree and every minute of cycle time counts, it removes a lot of the guesswork that older hydraulic machines quietly tolerate.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/